Race Time Jig
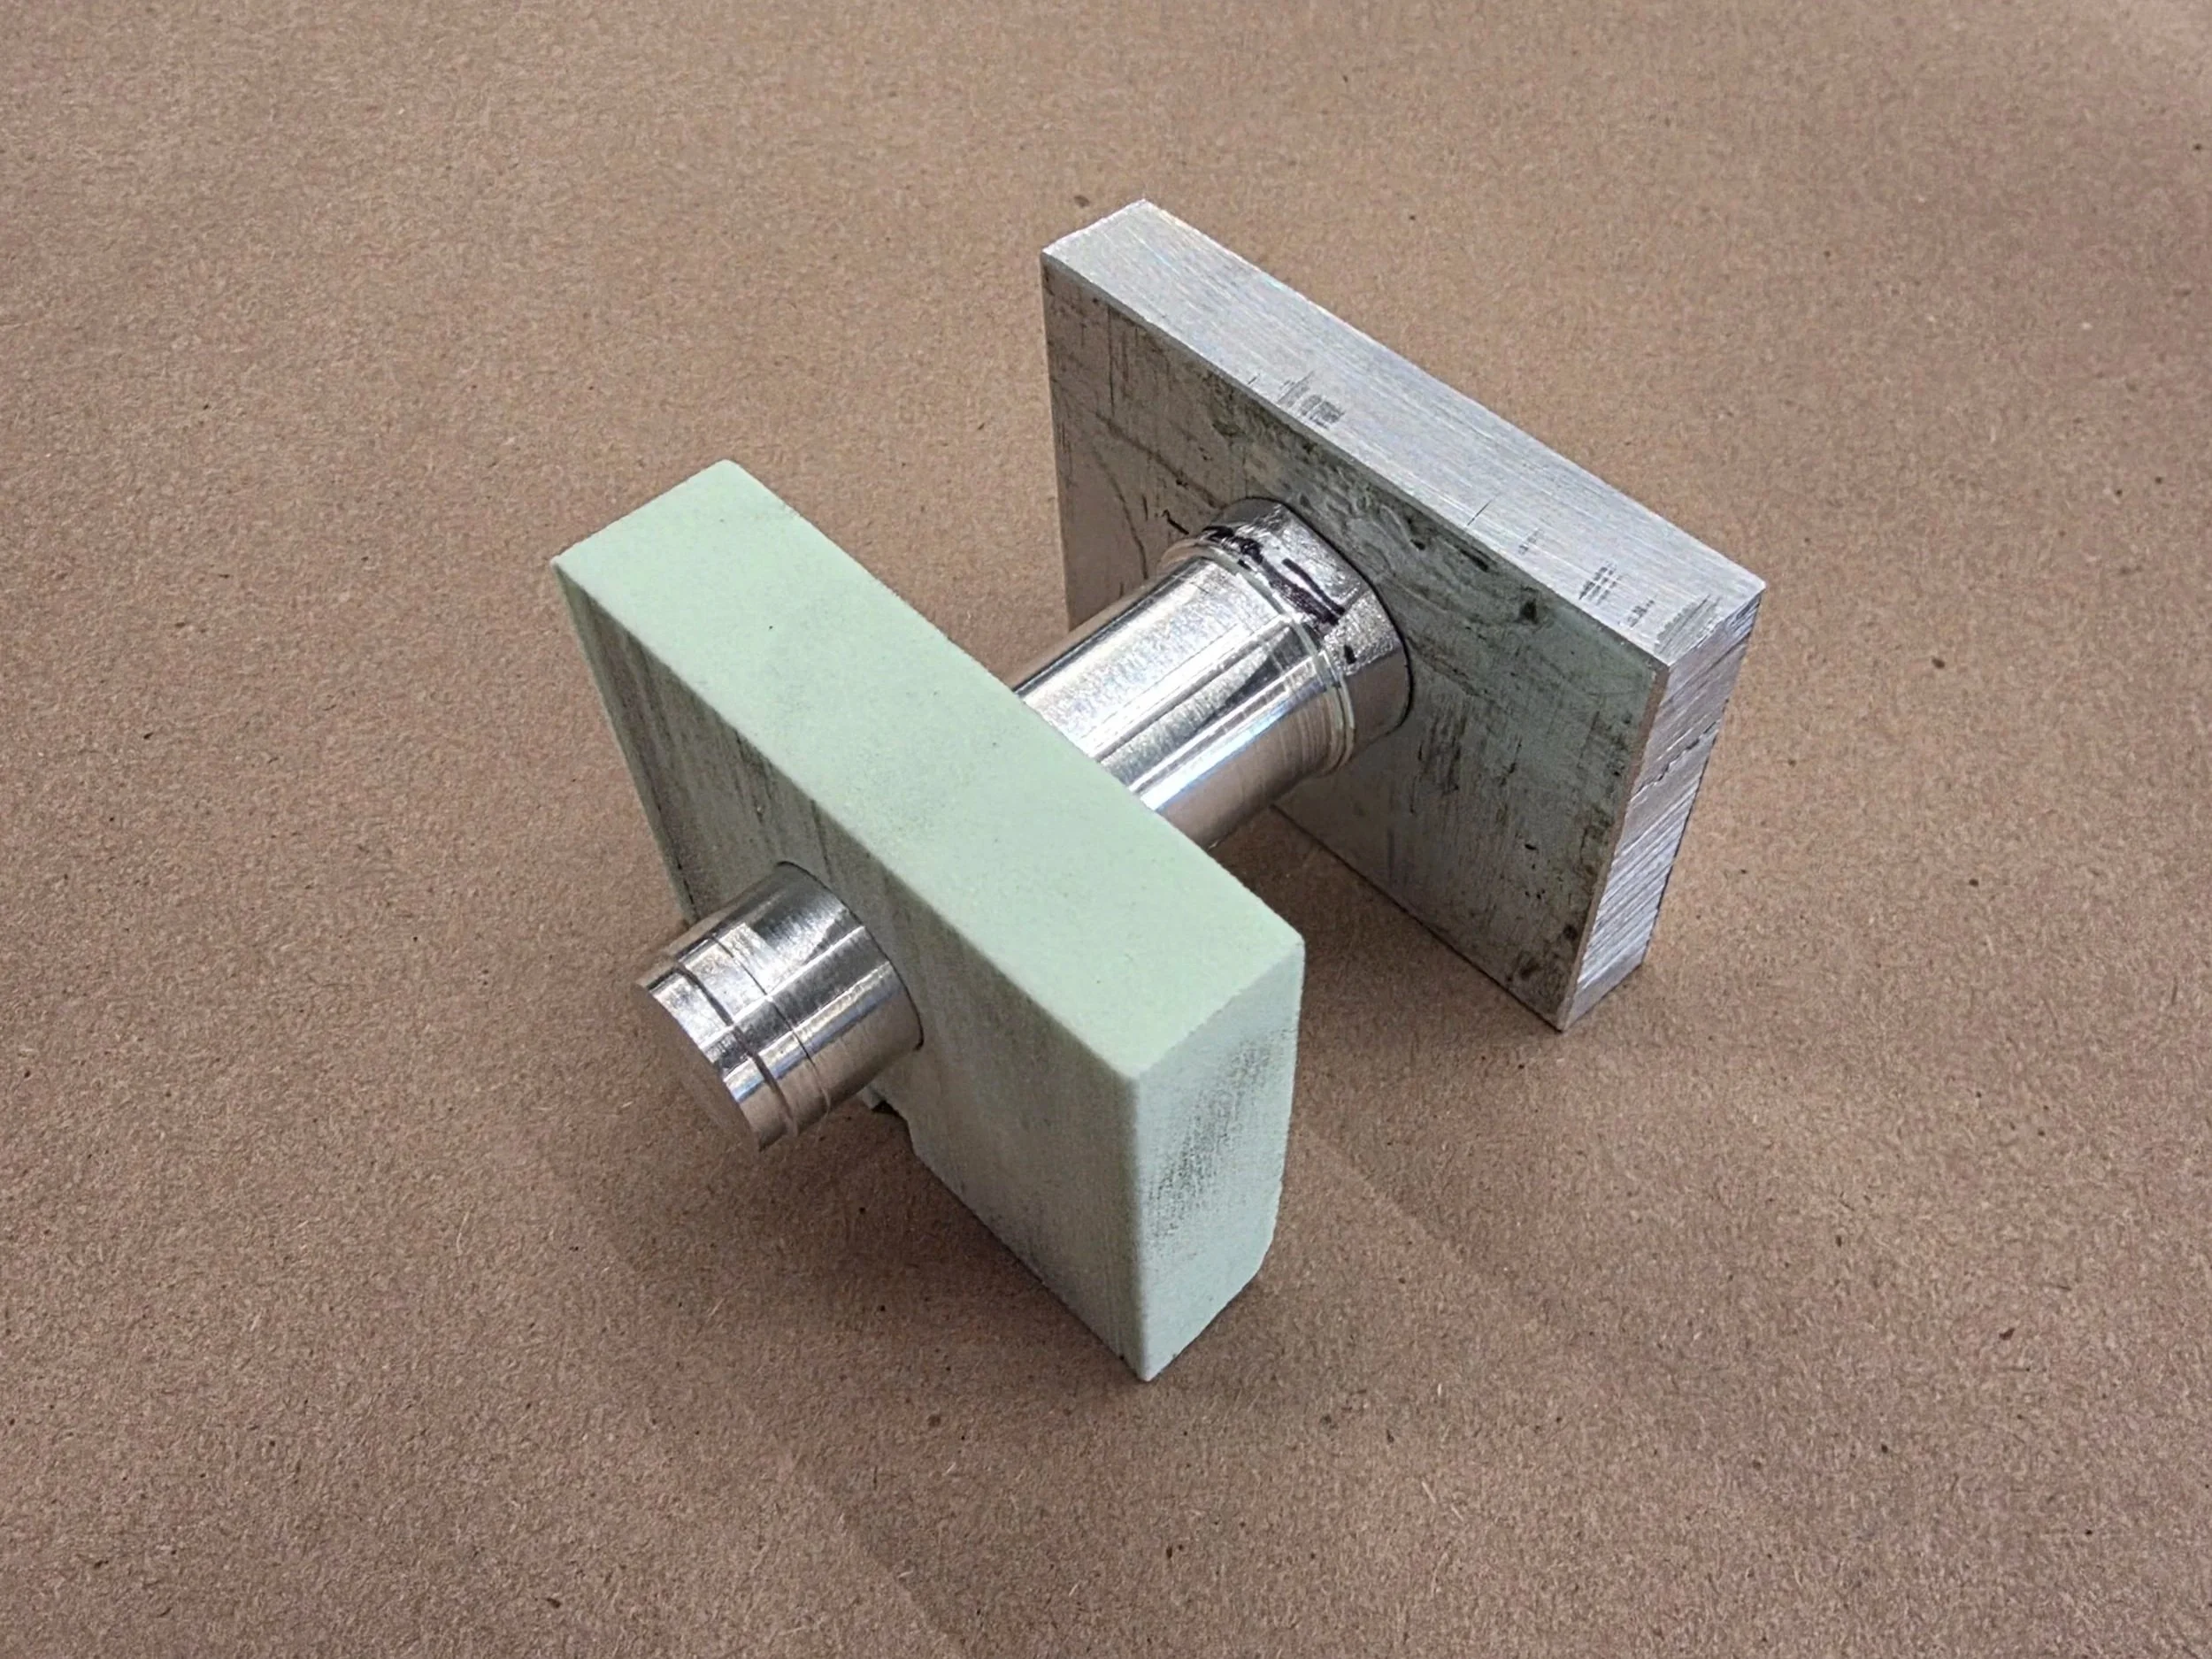
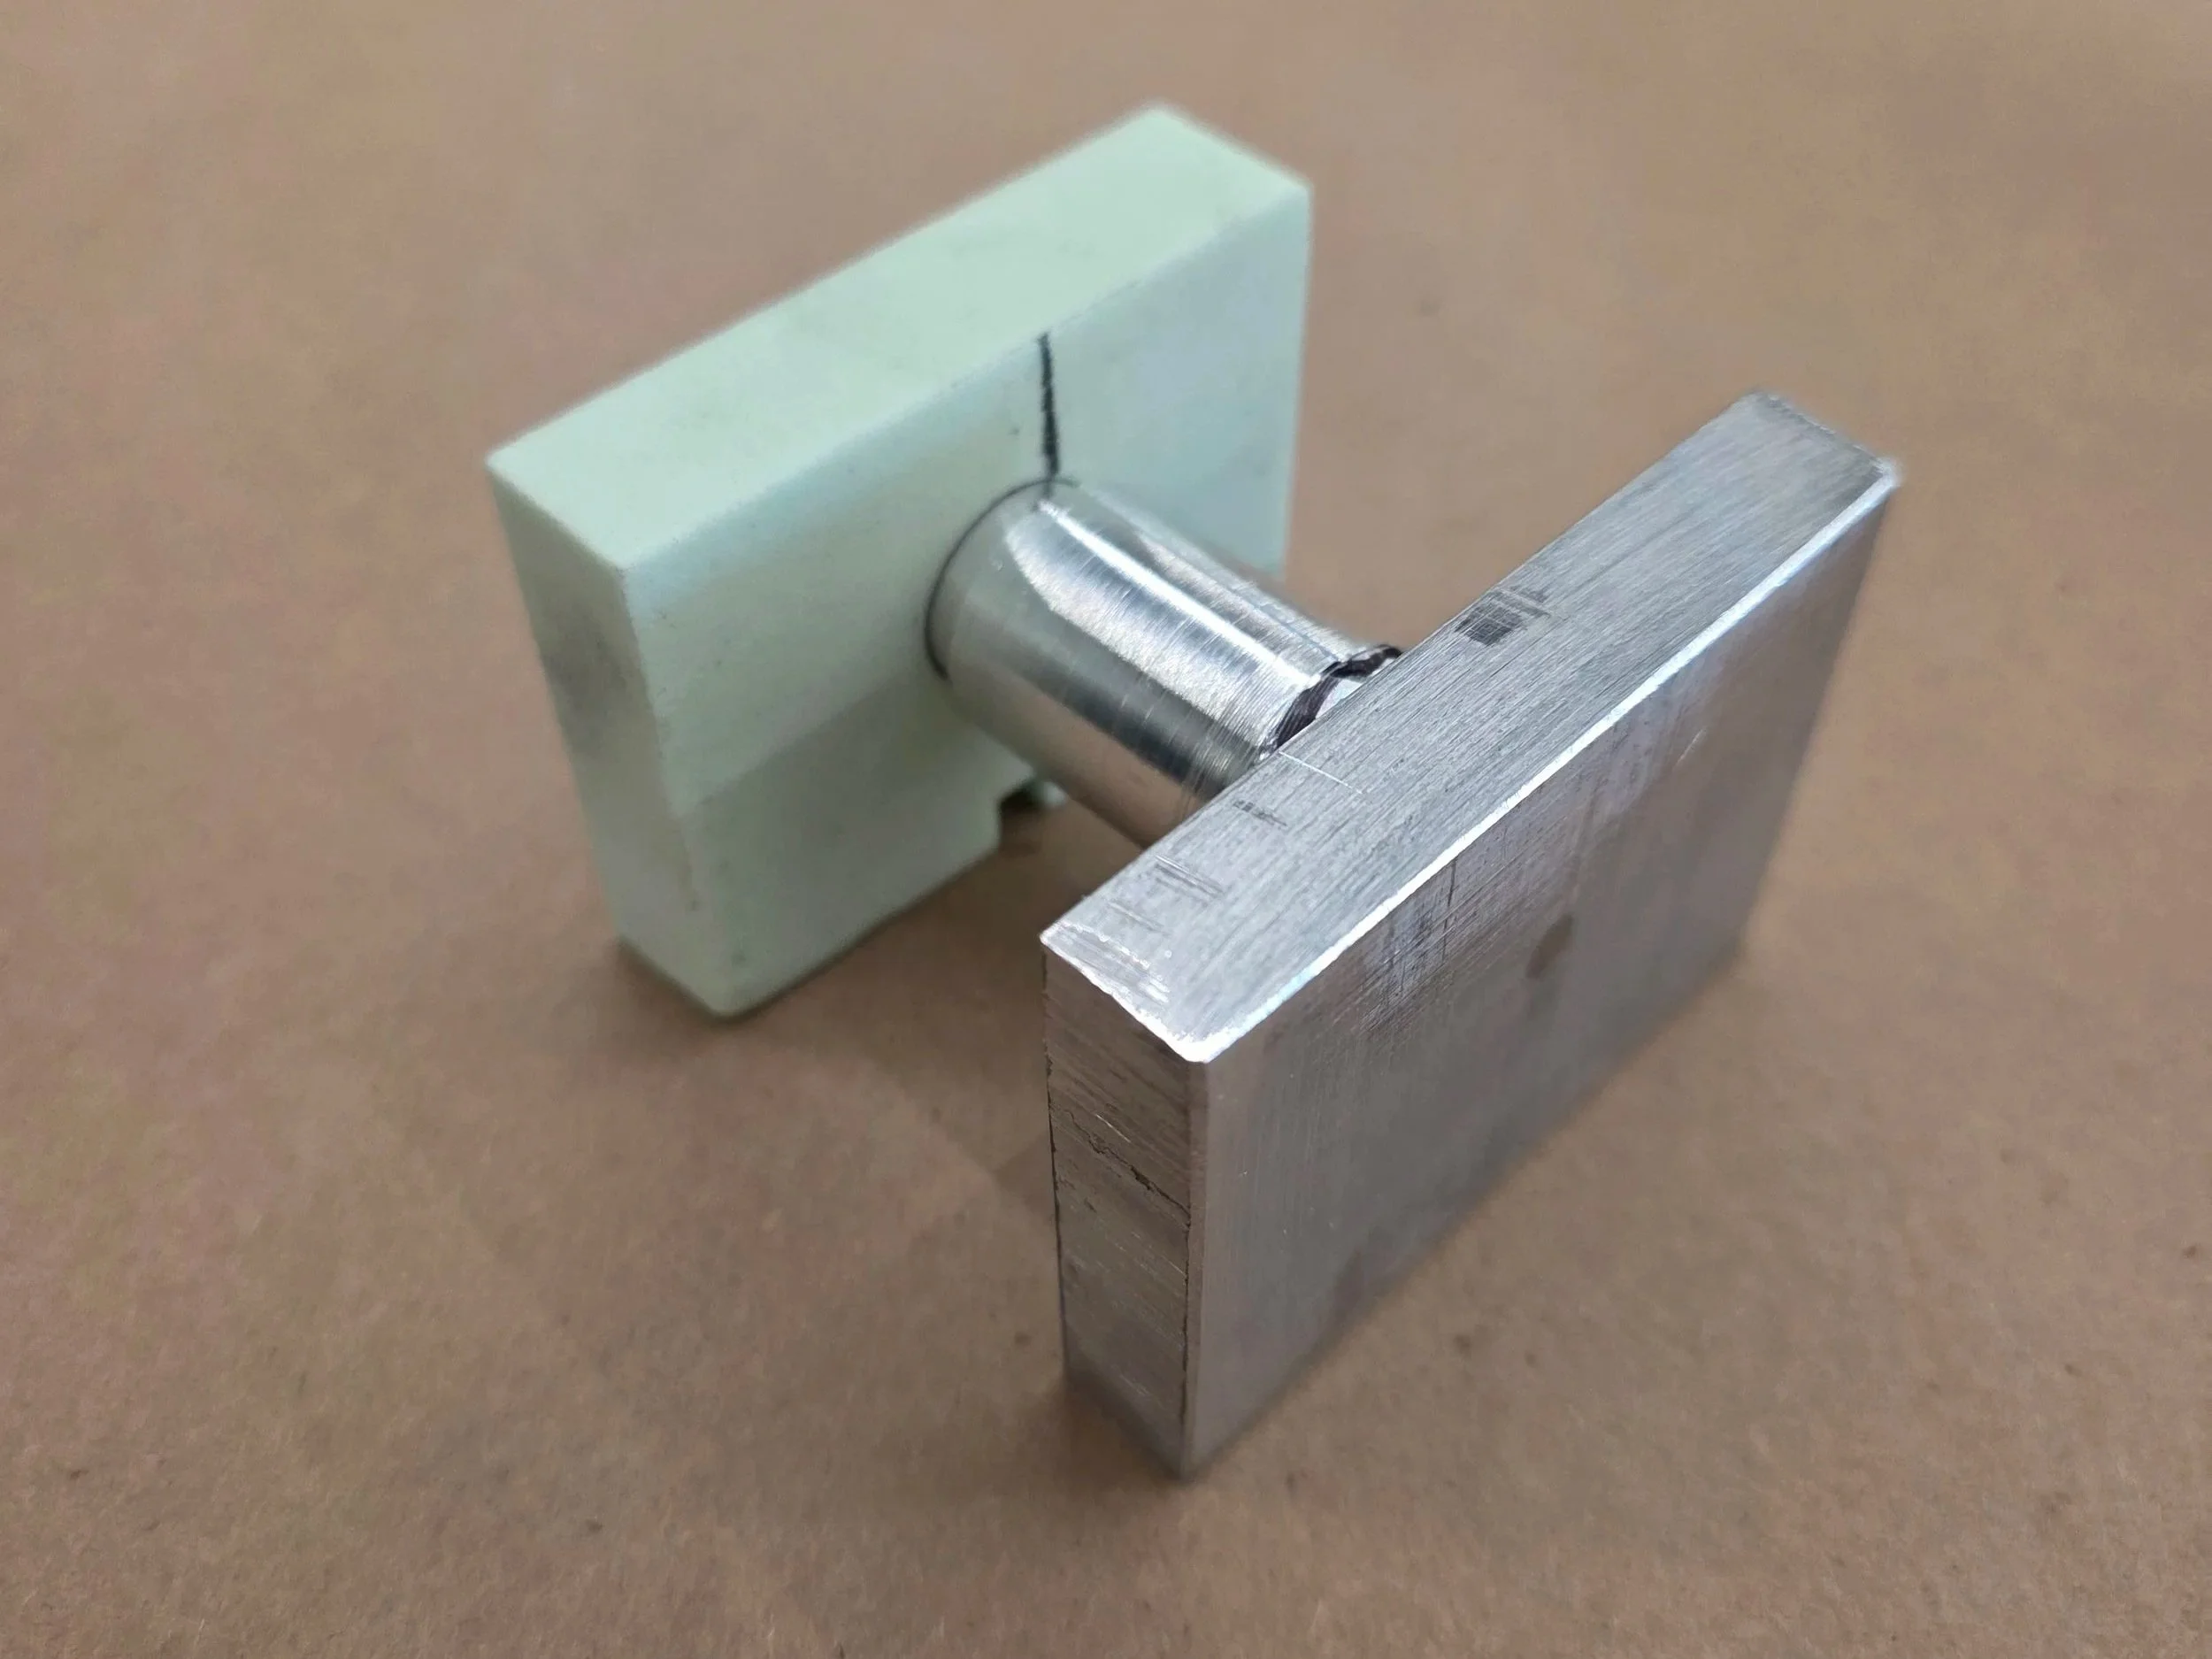
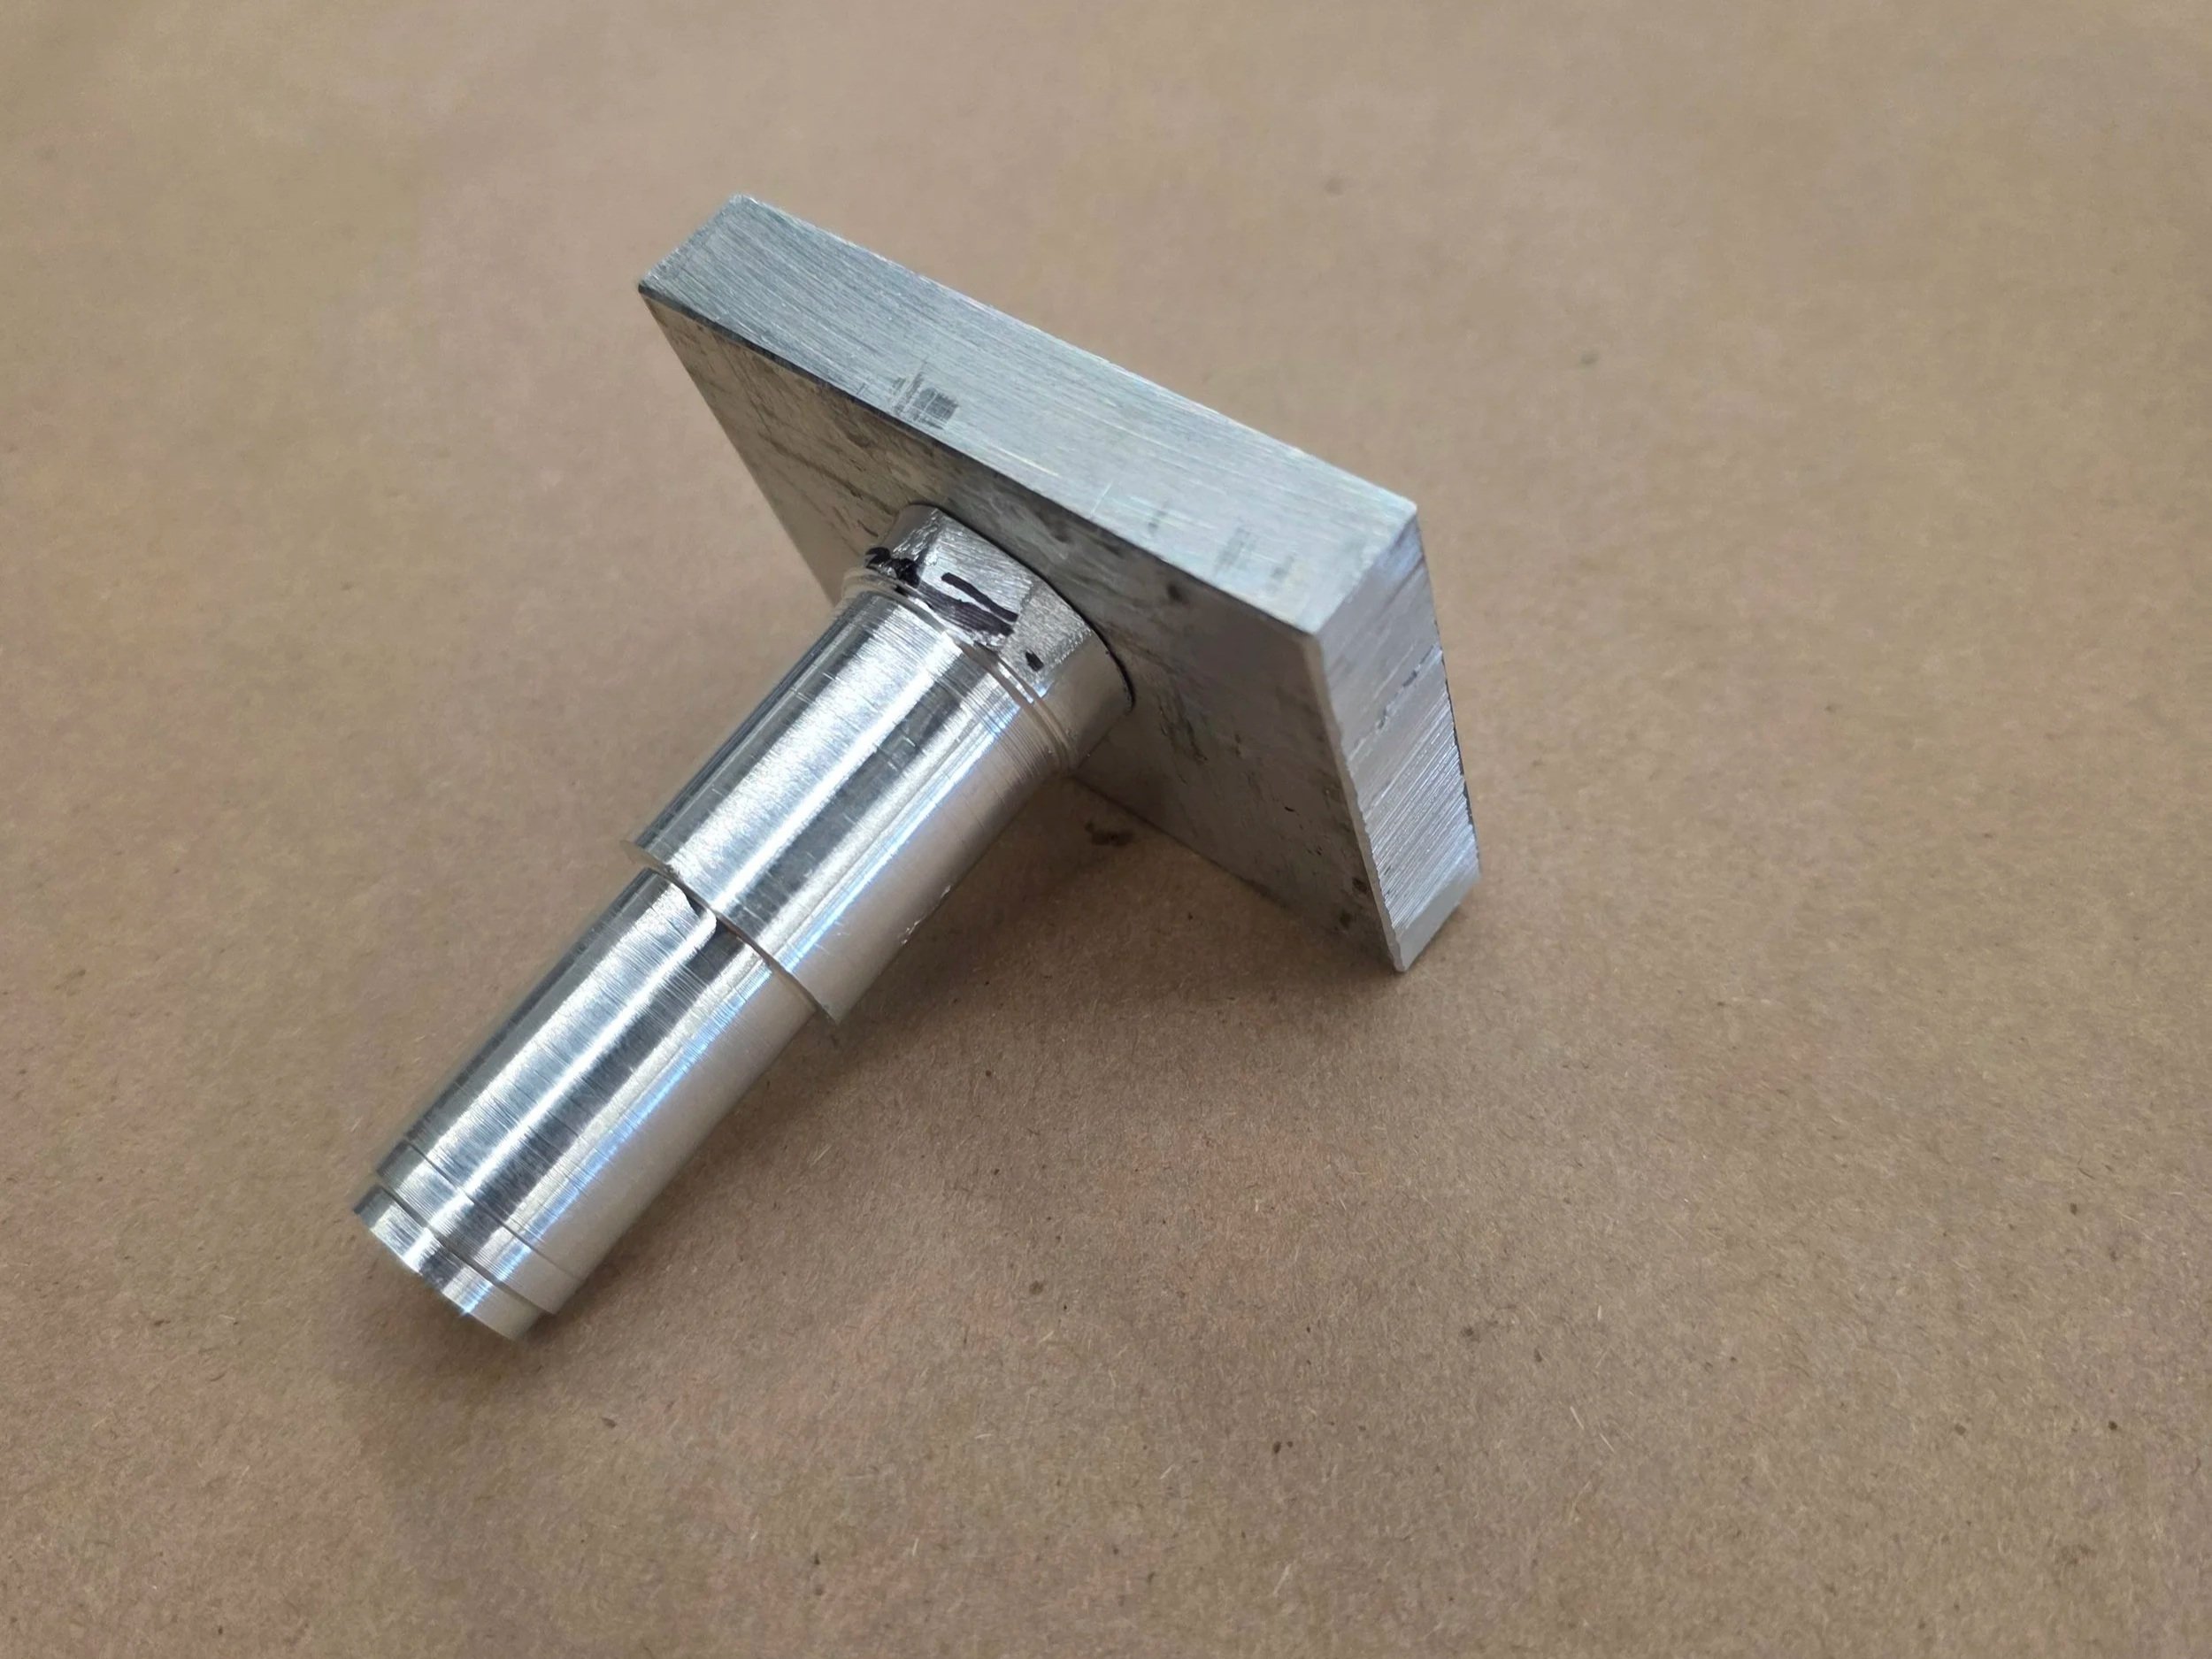
Engineered a custom modular holding fixture to process four high-density foam CO2 race car bodies under tight machining constraints. Designed for setup on a desktop Roland CNC router, the fixture compensated for a non-centered $Z$-axis cylinder bore alignment and the absence of a live tailstock. By securing the workpiece at precise datum points, the jig ensured repeatable part positioning, maintained tolerance compliance, and prevented stock deflection across long operational runtimes.
DFM & Process Optimization: Standardized stock orientation and localized clamping to eliminate tool deflection during deep-pocketing cuts, successfully maintaining dimensional accuracy across complex contours.
Root Cause & Failure Analysis: Identified a fundamental bottleneck in the baseline CAM workflow—the machine's auto-generated toolpaths required 6–8 hours per unit. Combined with hardware limitations and a 4-day delivery window, this yield rate made complete production physically unfeasible.
Engineering Takeaway: Highlighted the critical importance of performing capacity planning and machine capability analyses prior to commitment, prompting a pivot toward multi-axis setups and aggressive toolpath optimization strategies for future rapid-turn projects.